

Internal pipe coating is a factory-applied protective layer bonded to the inside wall of a steel pipe — distinct from external coating, and different from pipe lining. Steel pipes produced with this protection are commonly referred to as internal coating pipe in procurement specifications and supplier catalogs. Get the type wrong and your system either fails corrosion inspection or forces a full hydraulic recalculation at the job site. This article covers the three main coating types, where each applies in fire protection and industrial systems, and what to put in your purchase order to get exactly what you specify.
What Internal Pipe Coating Is — and What It Is Not?
Internal pipe coating is a chemical or mineral layer applied to the bore of a steel pipe to protect against corrosion, contamination, and friction loss from the fluid or gas flowing inside. Depending on the material, it runs between 200 and 600 microns thick and is bonded directly to the steel surface at the manufacturing stage.
External coating handles the outer wall — soil contact, atmospheric moisture, UV exposure. The two attack paths are independent. A pipe with a perfect external epoxy layer can still corrode from the inside in under five years if no internal coating is applied. Specifying one without considering the other is a common procurement gap.
The term is also routinely confused with internal lining. Coating refers to thin-film applications — typically FBE or liquid epoxy at 200–600 µm — chemically bonded to the steel surface. Lining refers to thicker structural barriers, most commonly cement mortar at 6–12 mm, which create a physical separation between the fluid and the pipe wall rather than a molecular bond. That distinction matters directly for hydraulic calculations: a cement lining reduces the usable bore, while an FBE coating at 400–600 µm has negligible impact on flow area. For a side-by-side breakdown of both methods, see pipe lining vs. coating: exact differences explained.
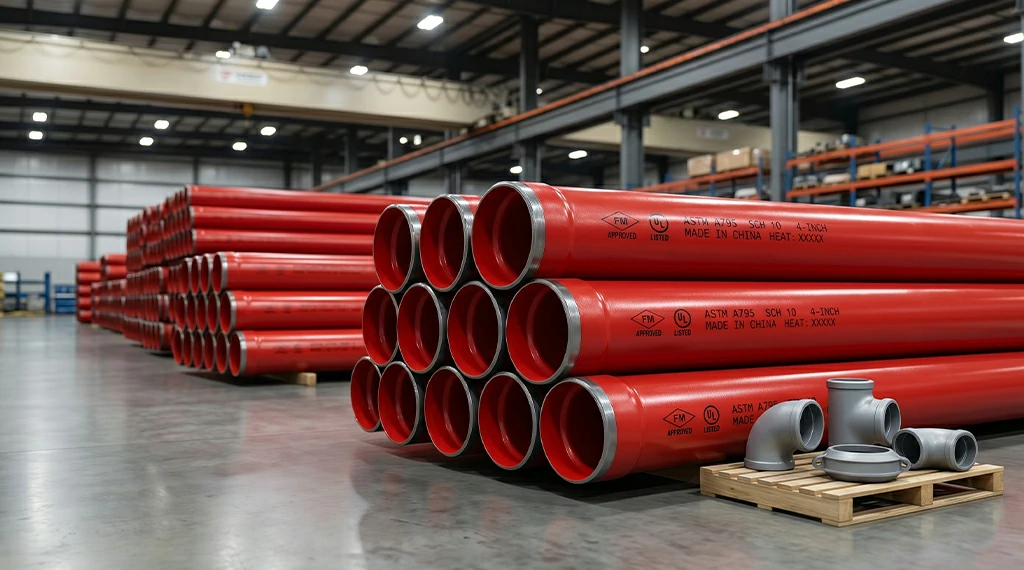
Three Types of Internal Pipe Coating and Where Each Fits
The three commercially dominant types cover most fire protection and industrial applications. The choice depends on operating temperature, the fluid being transported, and the applicable project standard.
| Type | Thickness | Temperature Range | Primary Application | Key Standard |
| Fusion Bonded Epoxy (FBE) | 400–600 µm | −40°C to 85°C | Fire protection, oil & gas, chemical | AWWA C213 |
| Liquid Epoxy | 200–400 µm | −20°C to 60°C | Field joints, repairs, food-grade lines | AWWA C210 |
| Cement Mortar Lining | 6–12 mm | 0°C to 70°C | Municipal water, sewage (DN300+) | AWWA C205 |
Fusion Bonded Epoxy (FBE)
FBE is a dry powder applied electrostatically to a preheated pipe surface — the steel is heated to 180–230°C and the powder melts and cross-links into a hard, continuous film. Pull-off adhesion strength typically exceeds 14 MPa, and the cured surface is smooth enough to measurably improve flow efficiency. FBE dominates fire sprinkler systems and buried gas transmission lines for these reasons. At 400–600 µm it is thick enough to resist mechanical damage during installation, yet thin enough that bore reduction is negligible — no hydraulic recalculation required.
Liquid Epoxy Coating
Liquid epoxy is a two-component system — resin and hardener mixed on site or in the factory, applied by brush or airless spray at 200–400 µm. It is thinner and less uniform than FBE at production scale, which makes it unsuitable for long runs of new pipe in bulk orders. Its value is flexibility: it can be applied to field welds, irregular fittings, and short pipe sections that cannot pass through a factory oven. Food-grade formulations are non-toxic and are used in pipes carrying potable water or food products. For large-volume new pipe procurement, liquid epoxy is rarely the right primary specification.
Cement Mortar Lining
Cement mortar is centrifugally spun inside the pipe and cures to a 6–12 mm rigid layer. It is cost-effective for large-diameter municipal water and sewage pipes (DN300 and above) where weight penalty is acceptable and bore reduction is designed into the hydraulics from the start. It is not suitable for fire sprinkler systems — the added weight, susceptibility to freeze-thaw cycling, and poor resistance to chlorinated or acidic media disqualify it from most building fire protection and industrial chemical applications.
Internal Coating Standards for Fire Protection Pipes
Fire protection systems carry the most explicit internal coating requirements of any building application. ASTM A795 governs ERW and seamless steel pipe used in sprinkler systems and permits black, galvanized, or FBE-coated finishes — but UL and FM approval listings increasingly favor FBE internally coated pipe, particularly for dry and pre-action systems.
The hydraulic implication is direct. An uncoated black steel pipe carries a Hazen-Williams C value of 100. An FBE-internally-coated pipe raises that to 140 — a 15% improvement in flow efficiency that can qualify a system for a smaller pump or reduced branch line diameters, partially offsetting the coating cost on a medium-sized project.
Galvanized pipe carries a specific failure risk in dry systems. Zinc particles shed from the galvanized layer under repeated pressure cycling and can obstruct sprinkler heads or orifices. Several FM-approved project specifications now prohibit galvanized pipe in dry systems for this reason. FBE internal coating does not shed particles and does not introduce that failure mode. In high-humidity coastal or tropical installations, uncoated black steel in a wet system can show pinhole corrosion within three years. For a full comparison of FBE-coated red fire pipe performance under UL and FM test conditions, see why epoxy-coated red pipes are the right choice for fire pipeline projects.
Industrial Systems Where Internal Coating Is Non-Negotiable
Fire protection is the most regulated use case, but industrial piping carries more varied demands. The correct coating type follows the transported medium, not the pipe material alone.
Chemical process piping requires confirmed compatibility between the epoxy formulation and the specific reagent. Standard FBE handles a broad range of industrial fluids, but aggressive acids and solvents require verification. Request the coating manufacturer’s chemical resistance table before specifying FBE for lines operating above pH 12 or below pH 4 — standard FBE loses adhesion under sustained exposure at those extremes.
Oil and gas transmission pipelines default to FBE for internal coating under API 5L and related standards. Beyond corrosion protection, the smooth FBE surface slows paraffin deposition in crude oil lines — a maintenance cost that compounds significantly over a pipeline’s operational life.
Large-diameter water transmission mains (DN300 and above) are the primary domain of cement mortar lining. The material cost advantage over epoxy is substantial at that diameter, and bore reduction is factored into the original hydraulic design. Below DN300, FBE is generally more practical because the proportional bore reduction from a 6–12 mm cement layer becomes hydraulically significant.
This is where most cross-sector procurement errors occur: applying municipal water pipe specifications to fire or industrial pipe, or vice versa.
How to Specify Internal Pipe Coating in a Purchase Order?
Writing “epoxy coated” in a purchase order is not a specification. A manufacturer can satisfy that description with a 200 µm brush-applied liquid epoxy that costs a fraction of factory-applied FBE — and the delivery note will say “epoxy coated” on both.
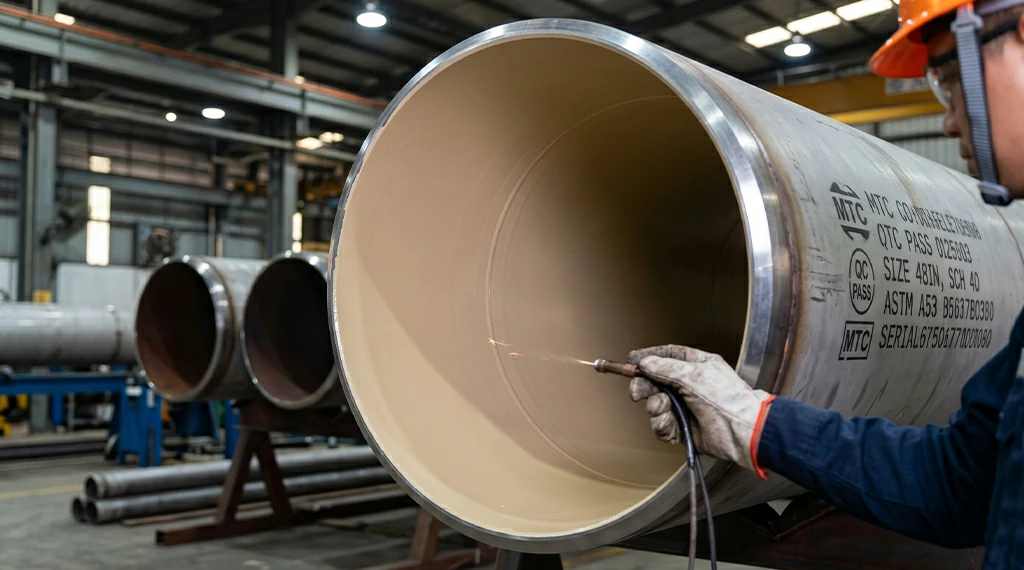
A complete internal coating specification requires six items: the coating type by name (FBE, liquid epoxy, or cement mortar); dry film thickness in microns with both a minimum and a tolerance range; the applicable standard by document number (AWWA C213 for FBE, AWWA C210 for liquid epoxy, AWWA C205 for cement mortar); curing method, whether factory oven or ambient cure; holiday test parameters, typically zero holidays at 67.5 V/µm for FBE; and whether the coating specification covers the internal bore only or includes weld seam coverage on ERW pipe. Each missing item is a gap a supplier can exploit without technically breaching the contract.
Mill test reports (MTR) with per-pipe coating thickness measurements and holiday test records close that gap. Baolai Steel’s factory-applied internal pipe coating solutions for fire and industrial systems cover liquid epoxy, single-layer FBE, and cement mortar lining, with full documentation packages available for each type.
About Baolai Steel
Founded in 1991, Baolai Steel manufactures seamless and ERW steel pipes, fire sprinkler pipes, and coated pipe systems from its facility in China. The factory holds ISO 9001, UL, and FM certifications and exports to more than 80 countries. Its internal coating pipe lines cover single-layer FBE, liquid epoxy, and cement mortar lining, applied and tested to AWWA and ASTM standards. Mill test reports, holiday test records, and coating thickness data sheets are available for every order. For procurement teams that need verified technical documentation alongside factory pricing, Baolai’s engineering team can provide specifications tailored to your project standard and volume.If you are sourcing internal coating pipe for a specific project, contact Baolai Steel’s team with your pipe size, coating type, applicable standard, and delivery volume — we will provide a factory price and full technical documentation within 24 hours.
Choosing the Right Internal Coating Starts with the Application
The coating type narrows quickly once the operating conditions are defined. FBE is the default for fire protection systems and most industrial piping below 85°C carrying water, gas, or moderate-pH process fluids. Cement mortar belongs on large-diameter water transmission mains where bore reduction is already in the design. Liquid epoxy handles the gaps — field joints, short replacement sections, and food-grade requirements that factory FBE cannot reach economically.
The specification document is where that choice either holds or gets quietly downgraded. A coating type written without a thickness tolerance and a referenced standard gives the factory room to substitute. An MTR with holiday test data and per-pipe DFT measurements confirms that what was ordered is what shipped. Before the next pipe order goes to the factory, check whether those two columns in the technical specification are filled in. They are the ones most likely to be blank.


