

ERW pipe is produced by forming a steel strip into a cylinder, heating its longitudinal edges with high-frequency current, and forging them together under squeeze pressure, generally without filler metal. The pipe then passes through weld flash control, any required seam heat treatment, cooling, sizing, cutting, inspection, finishing, marking, and packing.
The manufacturing method alone does not determine project suitability. Material identity, weld stability, dimensions, testing, and traceability must meet the applicable standard and purchase specification. Internal flash removal, seam heat treatment, hydrostatic testing, or third-party inspection may apply to some orders but not others.
This guide follows the process from specification review to final release, explaining what each stage controls, what buyers should confirm before production, and which records verify the delivered batch. The first step is defining the pipe’s service and acceptance criteria.
How Buyers Can Avoid ERW Pipe Specification Gaps Before Production?
Before requesting a quotation, first describe the pipe’s intended service. State whether it will be used for structural fabrication, general fluid transport, pressure service, or a pipeline. Buyers should also provide the conveyed medium, design pressure, operating temperature, corrosion conditions, and any planned processing such as bending, grooving, threading, or coating. These details help determine which product standard, grade, dimensions, and manufacturing controls may be suitable.
Next, identify the applicable standard. This requirement normally comes from the project drawings, engineering specification, end user, or local regulations. If it has already been selected, state the standard number, edition, and any project-specific amendments in the request for quotation (RFQ). If it has not yet been selected, submit the service conditions for technical review and obtain approval from the responsible engineer or end user before production. Similar dimensions or material grades do not necessarily make a structural pipe standard suitable for pressure or pipeline service.
After the intended service and applicable standard have been established, define the exact pipe requirements. These normally include the steel grade, outside diameter, wall thickness, length, dimensional tolerances, end finish, coating, marking, and packing. Buyers can then compare the available ERW steel pipe range against a consistent specification rather than requesting a general ERW pipe price.
ERW-specific manufacturing requirements should also be stated at this stage. Confirm the permitted internal and external weld flash, whether seam heat treatment is required, and whether later processing places additional limits on the weld area. These details can affect production planning, processing capability, and cost, so they should not be left until the pipe has already been manufactured.
Finally, define how compliance will be verified. The order should state the required nondestructive testing (NDT) method and coverage, hydrostatic and mechanical tests, inspection frequency, acceptance criteria, Mill Test Certificate (MTC), and any additional quality records. If third-party inspection (TPI) is required, include the hold, witness, and document-review points in the inspection and test plan (ITP) before production.
Once the service conditions, product specification, manufacturing requirements, and acceptance scope are aligned, the mill can prepare a production and inspection plan for the order.
ERW Pipe Manufacturing Process Step by Step
Once the specification and acceptance criteria are confirmed, production can begin. Coil and edge condition affect weld stability; post-weld processing affects final properties and dimensions; and inspection and traceability determine whether the batch can be released.
Coil Preparation and Edge Control
Production starts by checking the coil against the order and material certificate. The mill verifies the grade, properties, dimensions, surface, and heat number, which should remain linked to the production batch and pipe marking.
The coil is uncoiled and leveled so residual curvature does not disturb forming. On continuous lines, coil ends may be joined while an accumulator keeps the line operating. This joining weld differs from the longitudinal ERW seam and should be separately identified and controlled.
The strip is slit to width and checked for thickness, burrs, edge damage, and symmetry. Poor edges can disturb alignment, the welding V-angle, heat concentration, and squeeze pressure. Evidence may include incoming inspection records, heat-number traceability, and recorded strip dimensions.
Forming, Welding, and Weld Flash Control
After the strip width and edge condition have been accepted, successive forming rolls gradually bend the flat strip into an open cylindrical shape. During this stage, the mill controls strip tracking, edge alignment, roundness, and the V-shaped opening immediately before the welding point. Poor alignment can cause uneven heating or prevent the edges from bonding consistently.
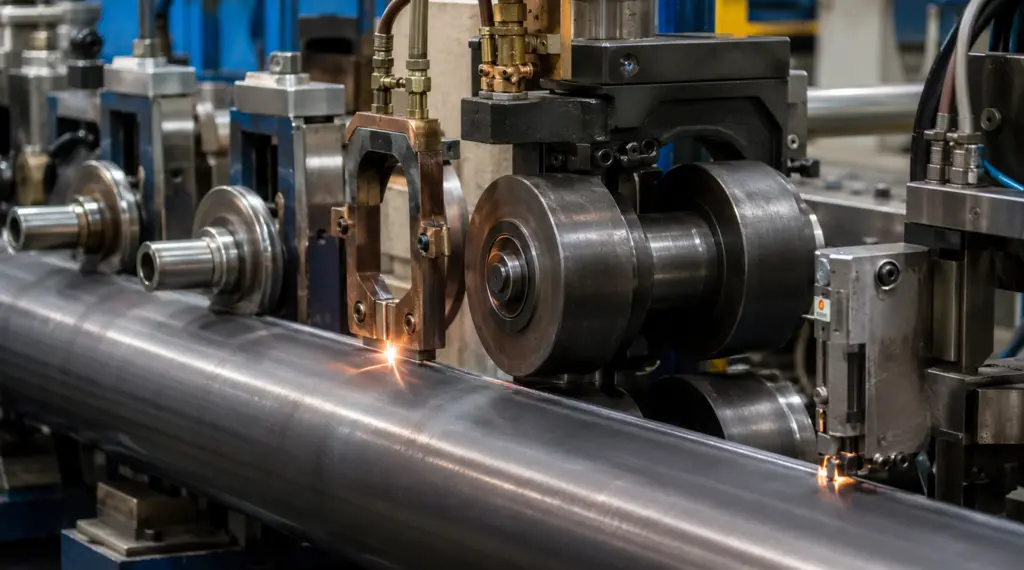
At the welding point, high-frequency current concentrates heat along the strip edges. Squeeze rolls then press the heated edges together to form a continuous longitudinal seam, generally without filler metal. Heat input, line speed, V-angle, edge alignment, squeeze pressure, and edge cleanliness must be controlled as one connected process. Unstable conditions may cause incomplete bonding, irregular weld upset, or inconsistent seam properties.
Squeeze pressure displaces a small amount of heated metal from the joint, creating weld flash on the outer and inner surfaces. External flash is normally trimmed to achieve the required surface condition, while internal flash may be removed or limited to a specified height depending on the applicable standard and purchase order. Internal flash control is particularly important when it may affect fluid flow, internal coating, grooving, or later machining.
After trimming, the weld area and remaining flash should be checked against the specified limits. The pipe can then proceed to any required seam heat treatment, followed by cooling and dimensional processing.
Heat Treatment, Cooling, Sizing, and Cutting
After welding and flash control, the pipe enters post-weld processing. Seam heat treatment or normalizing may be applied when required by the standard, grade, service, or order. Because it is not universal, its method, coverage, acceptance criteria, and records should be specified.
The pipe then passes through controlled cooling before sizing. A more stable temperature reduces thermal effects on diameter and roundness, supporting more consistent sizing and inspection. The cooling arrangement varies by line and specification.
Sizing rolls bring the pipe to the specified diameter and improve roundness. It is straightened where necessary and cut to length. Operators check diameter, wall thickness, ovality, straightness, length tolerance, and end squareness. Dimensional processing cannot correct an unacceptable weld.
Plain, beveled, threaded, or grooved ends are completed as ordered and checked for the specified dimensions and surface condition.
Final Inspection, Finishing, and Traceability
After sizing and cutting, the pipe moves to final acceptance and delivery preparation. Inspection has already occurred during material preparation and welding; final inspection brings the records together and confirms whether the finished pipe meets the order.
Required checks may include dimensions, surface condition, weld-seam NDT, hydrostatic testing, and mechanical testing. Their methods, coverage, frequency, and acceptance criteria should be defined in the order.
After product inspection, the specified coating or temporary protection is applied and checked. End protection, marking, bundling, and export packing follow. Final release should confirm that markings, inspection reports, the Mill Test Certificate (MTC), coating records, and packing documents refer to the same batch.
A complete traceability chain should therefore connect the coil heat number, production batch, pipe or bundle marking, inspection reports, MTC, and packing list. If one record cannot be matched to the others, the buyer may be unable to verify which material and test results apply to the delivered pipes.
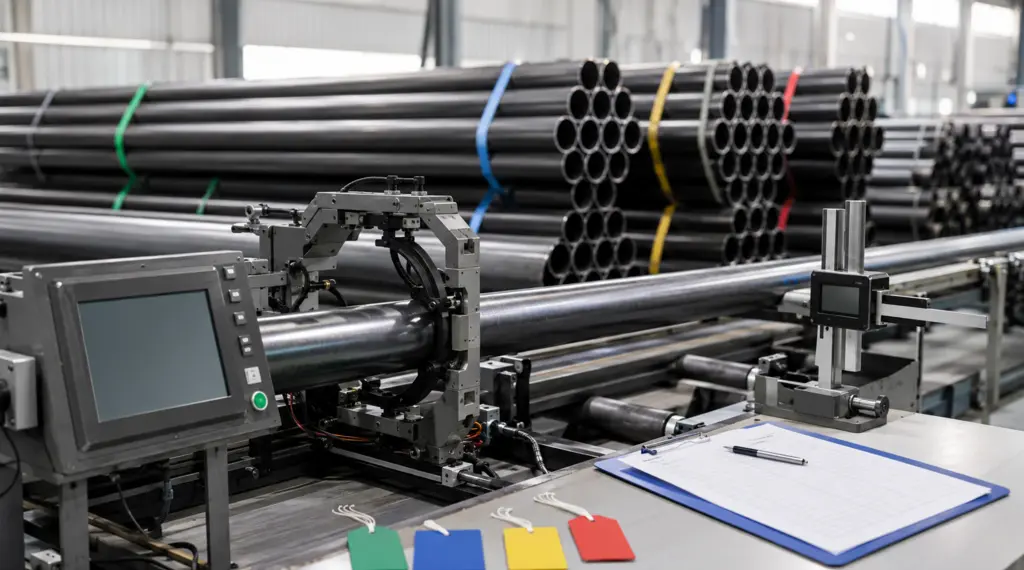
How ERW Pipe Quality Is Controlled and Verified?
ERW pipe quality cannot be established by one final test because incorrect material, weld-seam discontinuities, dimensional errors, and pressure leakage are different risks. Effective quality control assigns each risk an appropriate check and keeps the results traceable to the delivered batch.
Material control starts by matching the coil grade and heat number to the order, then carrying that identity through the production batch and finished pipe or bundle markings. Nondestructive testing cannot confirm that the correct steel grade was used, so the markings and Mill Test Certificate (MTC) must remain consistent.
The longitudinal seam requires additional control because its quality depends on connected variables such as edge alignment, heat input, line speed, V-angle, squeeze pressure, and weld flash condition. Ultrasonic or eddy-current testing may then examine the weld area for specified discontinuities. The order must define the test method, coverage, frequency, and acceptance criteria because a “passed NDT” statement has little value without the procedure and applicable limits. Visual appearance alone cannot confirm internal weld integrity.
The finished pipe is also checked for dimensions and surface condition. Hydrostatic testing, when required, confirms that the pipe withstands the specified test pressure and holding time without unacceptable leakage or failure, but it does not replace weld-seam NDT. Mechanical tests verify the properties of specified samples; they do not mean that every pipe length has been destructively tested.
Buyers should therefore ask not only what inspection equipment the mill has, but also which records will be supplied for their order. The MTC, dimensional report, NDT and hydrostatic test records where required, mechanical test results, applicable heat-treatment records, and pipe markings should carry matching heat or batch references. Any quality control that is critical to the project should be defined in the purchase order and inspection and test plan (ITP) before production.
What Buyers Should Specify Before Ordering?
To keep quotations technically comparable and make the agreed controls enforceable, the requirements should be carried from the RFQ into the quotation, purchase order, and ITP. Use this checklist to define what should be specified before production and what evidence should be required during inspection or delivery.
| RFQ Item | What Buyers Should State | Evidence to Require |
| Standard | Number, edition, and project amendments | Compliance statement |
| Pipe details | Grade, OD, wall thickness, length, and tolerances | Product data and dimensional report |
| Weld condition | Permitted internal and external flash | Inspection record |
| Heat treatment | Required method and acceptance criteria | Treatment record, if applicable |
| Testing | NDT, hydrotest, mechanical tests, and frequency | Relevant test reports |
| Traceability | Heat, batch, pipe, and bundle identification | MTC and marking photographs |
| Finishing | Ends, coating, marking, and export packing | Final inspection report |
| TPI | Hold, witness, and document-review points | Signed release note |
Before comparing prices, confirm that each supplier quoted the same testing, finishing, documentation, and inspection scope. A lower price may exclude internal flash removal, special tests, or witness points.
Do not treat product-page capabilities as confirmed order scope. Write conditional requirements into the purchase order or ITP. For TPI, define hold, witness, and document-review points before production.
This checklist assumes that ERW pipe has already been selected. If the manufacturing method has not yet been finalized, compare the operating conditions, dimensions, processing requirements, inspection scope, and total procurement cost before choosing between ERW and seamless pipe. The ERW vs. seamless pipe guide provides a more detailed selection framework.
Conclusion: How Buyers Can Verify the ERW Process?
Finished-pipe photographs and the description “high-frequency welded” are not enough to verify ERW pipe quality. Before placing an order, buyers should confirm that the material identity, manufacturing controls, required tests, inspection records, pipe markings, and delivery documents can all be traced to the same production batch.
A technically complete quotation should also show exactly what is included in the price, such as weld flash control, seam heat treatment where required, NDT coverage, hydrostatic or mechanical testing, end finishing, coating, documentation, and third-party inspection. Comparing quotations on the same technical basis helps reveal whether a lower-priced offer excludes required testing, finishing, documentation, or inspection services.
When preparing an RFQ, include the applicable standard, grade, outside diameter, wall thickness, quantity, end finish, coating, testing, and documentation requirements. If some specifications have not yet been finalized, also provide the intended service, pressure, temperature, processing needs, and destination. Including this information when you submit your ERW pipe requirements helps ensure that the proposed product, inspection scope, lead time, and price are based on the same project conditions before production begins.
FAQs
1. Can ERW Pipe Handle Sub-Zero Temperatures?
The manufacturing method alone does not determine low-temperature suitability. Check the minimum design temperature, grade, thickness, applicable code, and impact-toughness requirements. State the test temperature, sampling frequency, and acceptance criteria in the RFQ.
2. Is ERW Pipe Suitable for Sour Service?
The ERW manufacturing method alone does not establish suitability for an H₂S-containing environment. The specification may require controls for composition, hardness, seam heat treatment, hydrogen-induced cracking, or sulfide stress cracking. Confirm suitability from the service conditions and project requirements.
3. Can ERW Pipe Be Grooved or Bent?
Some ERW pipes can be roll-grooved or bent, but the procedure should account for grade, wall thickness, weld position, internal flash, deformation, and coating. After processing, inspect for cracking, ovality, wall thinning, seam damage, and coating damage.
4. How Should ERW Pipe Be Stored?
Store pipes above ground on suitable supports in a dry, ventilated area. Separate grades, sizes, and heat numbers, preserve markings, and protect ends and coatings. Avoid standing water, chemicals, soil contact, and handling that may cause damage.


