

Galvanized steel pipe can last for several decades. For building water systems, 40 to 70 years is often used as a general planning range, but it is not a guaranteed service life. Aggressive water chemistry, wet or chloride-rich soil, coastal exposure, damaged zinc coating, and poor joint protection can cause much earlier corrosion. In a dry, controlled environment with an appropriate hot-dip galvanized coating, the pipe may remain serviceable for longer.
The useful question for a project is therefore not only “How many years will galvanized pipe last?” but “What service life can this pipe achieve under the specified conditions?” Buyers and engineers should evaluate the coating, exposure environment, conveyed fluid, installation method, and inspection plan before selecting a galvanized steel pipe. The following factors provide the starting point for that assessment.
What Determines Galvanized Steel Pipe Lifespan?
Galvanizing protects carbon steel in two ways: the zinc coating forms a barrier between the steel and the environment, and it can provide sacrificial protection where small areas of steel become exposed. The protection lasts only while enough effective zinc remains. Pipe wall thickness affects the remaining structural life after corrosion begins, but it does not replace the need for a suitable coating.
It is also important to distinguish between time to first maintenance and total pipe service life. The first describes when coating repair or other maintenance may be needed; the second describes when the pipe no longer meets the project’s safety or performance requirements. These two points should not be treated as the same date.
Zinc Coating Thickness and Process
In the same exposure environment, a thicker, continuous zinc coating generally provides a longer period of protection. Coating thickness is usually reported in micrometers or mils, while coating mass may be stated in grams per square meter. Procurement documents should clearly identify which value is required rather than using the terms interchangeably.
The galvanizing process also matters. Batch hot-dip galvanizing, continuous galvanizing, and electro-galvanizing can produce different coating structures and thicknesses. Buyers should specify the applicable pipe or galvanizing standard, minimum coating requirement, test method, and acceptance criteria. A standard should not be selected by name alone; it must match the product form, manufacturing process, and intended service.
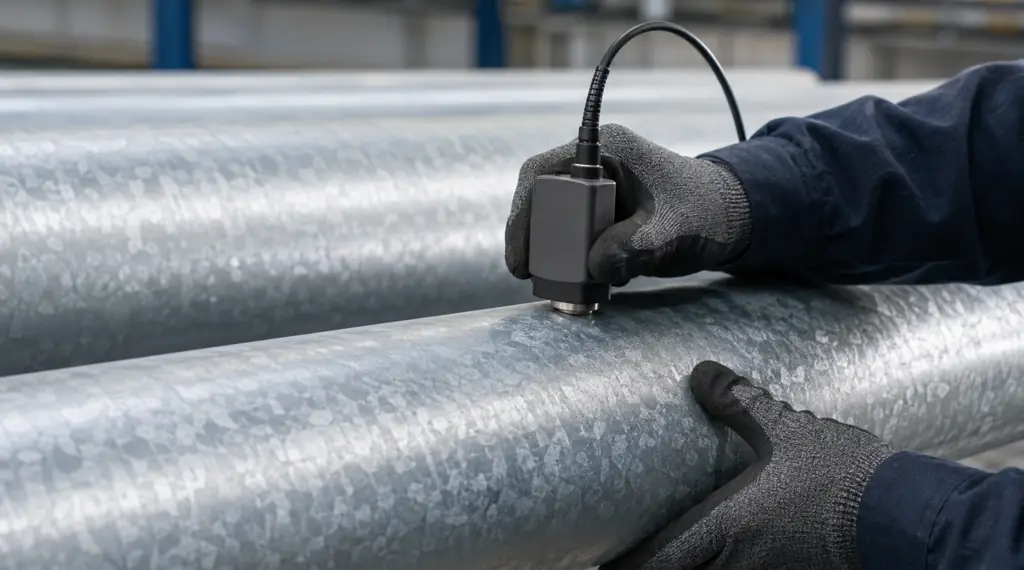
Before installation, inspectors can use a calibrated magnetic gauge to check coating thickness at representative locations. They should also look for bare spots, damaged areas, poor drainage details, and coating defects that could create localized corrosion.
Soil, Water, and Atmospheric Exposure
The surrounding environment controls how quickly zinc is consumed. For buried pipe, important factors include soil moisture, pH, chloride content, resistivity, drainage, and variations along the pipeline route. Dense, water-retaining soil can create a different corrosion risk from dry, well-drained soil, even within the same project.
For water service, temperature, dissolved oxygen, pH, alkalinity, chlorides, sulfates, and flow conditions all influence internal corrosion. Soft water can be aggressive toward zinc, while mineral-rich water can contribute to scale buildup and reduced internal diameter. Neither “soft” nor “hard” water alone is enough to predict service life; a water analysis is more useful than a broad label.
In atmospheric service, humidity, time of wetness, industrial pollutants, and airborne salt are key considerations. Coastal exposure should be evaluated by actual salinity and site conditions rather than distance from the shoreline alone.
Installation and Joint Protection
Installation damage can shorten the life of a correctly specified pipe. Dragging pipe across abrasive surfaces, using unprotected lifting methods, or allowing cut edges to remain exposed can remove zinc before the system enters service.
Threading, cutting, welding, and field modification also disturb the protective coating. The affected areas should be repaired or sealed using a method permitted by the project specification and applicable standard. When welded steel pipes are galvanized or coated for a project, the weld area, pipe ends, and field joints require the same inspection attention as the main pipe body.
Good installation practice also includes compatible supports and fittings, drainage where required, isolation from dissimilar metals when galvanic corrosion is possible, and careful repair of handling damage before commissioning.
How Long Does Galvanized Pipe Last in Different Environments?
Published lifespan figures are useful for early planning, but they should not be used as a warranty or final design value. The same galvanized pipe can perform very differently when the coating specification, fluid, or exposure condition changes.
Indoor and Water Service
In dry indoor structural service, galvanized pipe can remain usable for many decades because it is not continuously exposed to water, soil, or salt. A service life of more than 50 years may be achievable when the coating remains intact and condensation is controlled.
For building water systems, 40 to 70 years is a commonly cited planning range. Actual performance may be shorter where hot or chemically aggressive water accelerates corrosion, or where internal scale restricts flow. Industrial water systems need a separate evaluation because the conveyed fluid, operating temperature, pressure cycles, and shutdown periods may differ substantially from ordinary building plumbing.
Stagnant or low-flow sections in fire sprinkler pipe systems can face localized corrosion risks, but continuous flow is not a general solution for every fire protection system. Material selection, water quality management, correct system configuration, and inspection should follow the applicable fire protection standard and project requirements.
Underground and Buried Service
There is no reliable universal lifespan of 10 to 30 years for all buried galvanized pipes. Some installations may fail within that period under aggressive conditions, while properly specified hot-dip galvanized steel can last much longer in favorable soil. The difference depends on soil properties, coating thickness, mechanical damage, groundwater conditions, stray current, and any supplementary corrosion protection.
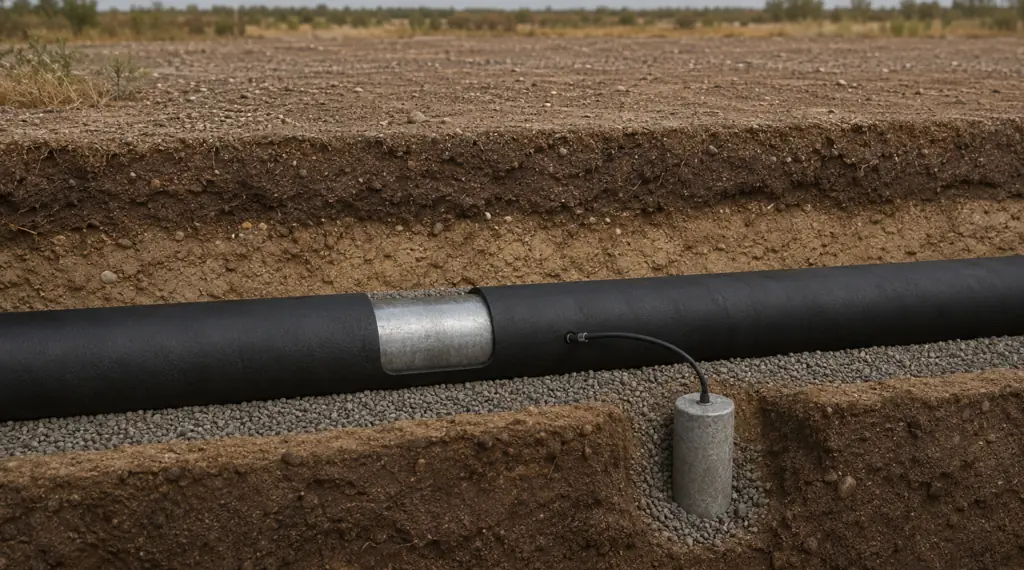
Before specifying buried pipe, the project team should test representative soil conditions along the route rather than relying on a single pH reading. Where the soil is highly corrosive, the design may require a compatible external barrier, engineered backfill, electrical isolation, or cathodic protection. Adding clean sand alone should not be assumed to solve every drainage or corrosion problem.
Coastal and High-Humidity Service
For galvanized pipe exposed to coastal air, approximately 20 to 50 years may be used as a preliminary planning range. Actual service life may be shorter near the shoreline or in areas with frequent salt spray, condensation, poor drainage, or coating damage. Direct seawater and continuously wet conditions require a separate assessment.
For severe coastal projects, buyers should confirm the zinc coating thickness, site exposure level, drainage conditions, and inspection schedule. A compatible duplex coating system may also be needed where standard galvanizing alone cannot provide sufficient protection.
How to Extend Galvanized Pipe Service Life?
Extending service life begins at the specification stage. Maintenance cannot fully compensate for an unsuitable coating or material selected for the operating environment.
Specify and Verify the Coating
Do not treat “galvanized” as a complete coating specification. Buyers should confirm the galvanizing process, applicable standard, minimum zinc coating thickness or mass, test method, and acceptance criteria. These details make it easier to compare suppliers and estimate whether the coating is suitable for the expected environment.
For aggressive atmospheric, buried, or industrial exposure, galvanizing alone may not provide sufficient protection. A compatible external coating over the zinc layer can form a duplex system, but surface preparation and coating compatibility must be verified. Understanding how external pipe coating options differ for buried and industrial service can help buyers compare FBE, 3LPE, 3LPP, and galvanized systems before finalizing the coating specification.
Consider Cathodic Protection for Buried Pipe
Cathodic protection is commonly used to help control corrosion on buried metallic pipelines. It supplies electrical current that shifts the pipe’s electrochemical potential, making corrosion less likely. Depending on the pipeline and soil conditions, the system may use sacrificial anodes or an external impressed-current power source.
When properly designed, cathodic protection can help protect exposed steel at small coating defects and extend pipeline service life in corrosive soil. It is generally used together with a suitable external coating rather than as a replacement for one. However, poor design or excessive current may reduce protection effectiveness, affect some coatings, or interfere with nearby metallic structures. A corrosion specialist should therefore assess the pipeline conditions, electrical continuity or isolation requirements, and monitoring plan before the system is selected.
Control Damage and Monitor Condition
Protect pipe during transport, storage, cutting, and installation. Repair coating damage using approved procedures, and document repaired locations for later inspection.
During service, use an inspection plan suited to the application. Useful methods may include visual examination, coating-thickness checks, ultrasonic wall-thickness testing, water-quality monitoring, pressure or flow trending, and targeted internal inspection. Flushing should follow the system design and maintenance procedure; excessive pressure or an unsuitable cleaning method can create additional risk.
Warning Signs Galvanized Pipes Need Inspection
The following symptoms do not always mean that the entire system needs immediate replacement, but they justify a closer condition assessment:
- Red rust or flaking corrosion: Red rust indicates that the underlying steel is exposed in at least part of the affected area. It does not necessarily mean the zinc coating has disappeared everywhere.
- Persistent white corrosion products: Light white staining may be superficial, but heavy or recurring white rust can indicate prolonged wet storage, poor drainage, or inadequate ventilation.
- Reduced pressure or flow: Internal corrosion and scale may restrict the bore, although pumps, valves, filters, and other system components should also be checked.
- Brown or red water: Discoloration can be associated with internal corrosion, but water testing and system inspection are needed to identify the source.
- Repeated leakage at joints or localized areas: Increasing repair frequency may indicate joint damage, galvanic corrosion, coating failure, or broader wall loss.
- Measured wall-thickness loss: Inspection readings that approach the project’s minimum allowable wall thickness require an engineering decision on repair, derating, or replacement.
Replacement decisions should be based on measured condition, remaining wall thickness, leak history, operating pressure, water or soil data, and the governing code—not on pipe age alone.
Conclusion
For procurement, define the operating environment first, then confirm the pipe standard, steel grade, wall thickness, galvanizing process, coating requirement, end finish, inspection method, and required documentation. If you are comparing galvanized steel pipe options for a live project, share the application, service environment, required standard, dimensions, quantity, and destination. Baolai Steel can then assess whether standard galvanizing is suitable, whether additional coating protection should be considered, and which inspection documents should be included before preparing a project-specific quotation.
FAQs
1. Can Galvanized Steel Pipes Be Used for Hot Water?
They may be used only when the pipe specification, water chemistry, operating temperature, and applicable code permit it. Accelerated corrosion through polarity reversal can occur in certain water conditions, particularly within approximately 60°C to 82°C (140°F to 180°F), but temperature alone does not determine whether it will occur. For a hot-water project, verify the full water analysis and system requirements rather than applying a universal yes-or-no rule.
2. Can Galvanized Pipe Connect Directly to Copper?
Direct contact between galvanized steel and copper in the presence of an electrolyte can increase galvanic corrosion risk. Use a code-compliant transition method, such as an appropriate dielectric fitting or other engineered isolation detail, and confirm compatibility with the conveyed fluid, pressure, and temperature. The connection should follow the project specification and local plumbing or piping code.
3. How Does MIC Affect Galvanized Pipes?
Microbiologically influenced corrosion, or MIC, can contribute to localized attack where microorganisms, deposits, water chemistry, and suitable operating conditions interact. Stagnant or low-flow areas may be more vulnerable, but MIC cannot be confirmed from appearance alone. Deposits, tubercles, or recurring pinhole leaks should prompt sampling and a system-specific corrosion assessment before choosing a treatment or replacement plan.


