

A galvanized steel pipe inspection should determine whether the material matches the purchase order and can be installed without avoidable corrosion, leakage, or connection problems. A bright surface is not enough; the coating, dimensions, tests, markings, and documents must refer to the same production batch.
The sequence matters. Establish the acceptance standard, inspect the coating and pipe, and then verify traceability. This prevents inspectors from judging a visible irregularity without knowing the contractual requirement.
What Should Be Confirmed Before the Inspection Begins?
Start with the purchase order. Confirm the standard and edition, grade, dimensions, galvanizing process, end finish, coating requirement, tests, sampling plan, and document package. If anything is unclear, obtain written clarification rather than inventing an acceptance limit on site.
A pipe standard and a coating standard may control different parts of an order. ASTM A53 covers welded and seamless black or hot-dip galvanized pipe, while ASTM A795 applies to fire-protection pipe. EN 10255 may be paired with EN 10240 for tubes galvanized in automatic plants.
ASTM A123 and ISO 1461 are not universal pipe standards. Pipes processed on specialized or automatic lines may fall under product-specific requirements. Prepare this reference sheet before production:
| Requirement | Approved reference | Inspector action |
|---|---|---|
| Pipe grade and dimensions | Product standard and PO | Check markings and measurements |
| Zinc coating | Product or coating specification | Confirm method, sampling, and limit |
| Pipe tests | Product standard and ITP | Review traceable reports |
| Surface acceptance | Agreed specification | Record defect and disposition |
| Packing and documents | PO | Match bundle data to certificates |
Also identify whether the pipe is hot-dip galvanized after manufacture or formed from pre-galvanized strips. The latter needs closer inspection at its weld seam and cut edges.
If the project has not fixed its corrosion-protection system, reviewing the available coated pipe solutions can help the buyer compare galvanizing with other internal and external coatings before defining the inspection criteria.
How Should the Zinc Coating Be Checked?
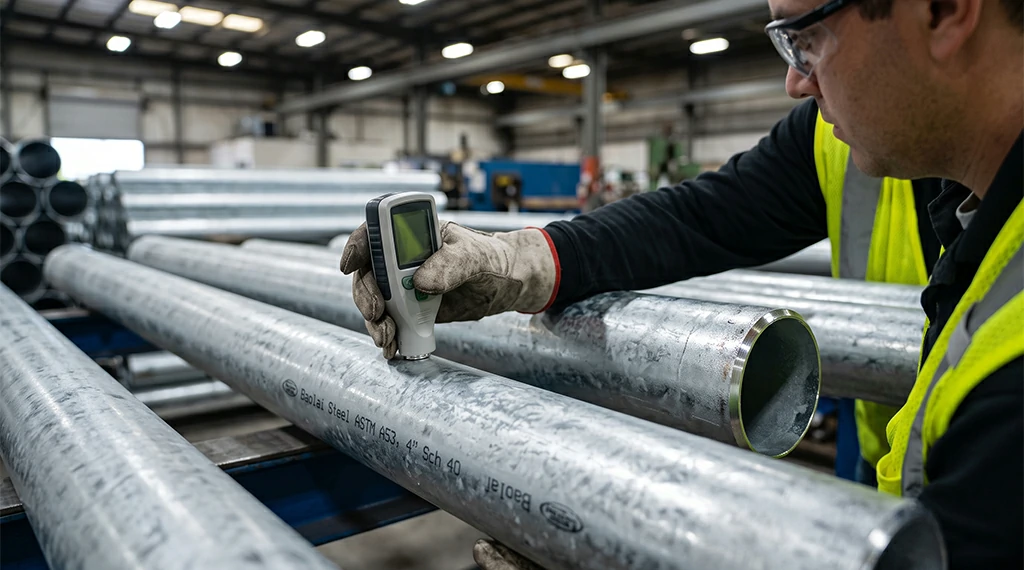
Begin with coverage, then measure quantity. Inspect the external surface, bore near both ends, seam, pipe ends, threads, grooves, bundle contact points, and lifting marks. The coating should be continuous and connections unobstructed.
Measure coating thickness with a calibrated magnetic or electromagnetic gauge. Curvature, roughness, and poor calibration can distort readings, so measure agreed positions around the circumference and length, including the seam and ends. Record the bundle, gauge, calibration, readings, average, requirement, and result.
If a reading is low, confirm calibration, repeat it, and expand sampling. An isolated low area may be repairable; a repeated batch-wide shortfall normally requires reprocessing or rejection.
The acceptance value must come from the order. Statements such as “every galvanized pipe requires 85 μm” ignore differences between standards, pipe types, and service conditions. Buyers still defining these requirements can compare Baolai’s galvanized steel pipe options before fixing the inspection plan.
Which Surface Defects Need Corrective Action?
Appearance should be judged by its effect on corrosion protection and use, not by colour alone. The following table connects each condition with a practical response.
| Surface condition | Risk | Corrective action |
|---|---|---|
| Bare spot | Base steel is exposed | Measure the area; repair within the standard limit or regalvanize |
| Peeling or flaking | Coating adhesion has failed | Isolate affected pipes and rework or reject |
| Blister | Zinc may be separated from the steel | Check adhesion and the extent of the defect |
| Flux deposit | Residue may retain moisture | Clean without damaging zinc, then reinspect |
| Zinc lump or run | May obstruct threads, grooves, or fittings | Smooth safely and verify coating and fit |
| Scratch or handling mark | Local protection may be reduced | Measure remaining coating and repair if required |
| White storage stain | Severity ranges from superficial to damaging | Dry and clean; measure the coating if heavy |
| Dull or mottled finish | Usually an appearance variation | Accept if coverage and coating requirement are met |
Small zinc-covered dross particles and a dull grey finish may remain serviceable. Rejecting them solely for appearance can waste compliant material.
White storage stain requires a measured response. Light staining often develops when moisture is trapped between bundled pipes and may not materially reduce protection. Heavy deposits should be removed so the zinc beneath can be measured. If cleaning reveals bare steel or inadequate coating, repair or reject the pipe; if the coating remains compliant, improve ventilation and repack the material dry.
Functional areas require stricter judgement. After removing a zinc run from a thread or groove, use a gauge or fitting trial to confirm that the connection still works.
Which Pipe Dimensions and Tests Must Be Verified?
Galvanizing cannot correct a thin wall, damaged end, or defective weld. Measure outside diameter, wall thickness, length, straightness, and ovality where specified. For threaded, grooved, or beveled pipe, check the dimensions that control the joint rather than relying on appearance.
Use a calibrated caliper for outside diameter, an ultrasonic gauge for wall thickness where appropriate, and approved gauges for threads and grooves. If excess zinc prevents measurement, remove only the permitted obstruction and recheck the area so dimensional correction does not leave exposed steel.
Measure wall thickness at several points. For a low result, clean the area, verify the instrument, repeat the reading, and expand the sample. Consistent shortfalls indicate a manufacturing problem and should not be averaged away.
Testing also follows the product specification. The official ASTM A53/A53M specification, for example, covers welded and seamless black and hot-dip galvanized pipe and includes material, mechanical, and pipe-integrity requirements. Depending on the order, the inspection package may include chemical analysis, tensile properties, flattening or bend tests, hydrostatic testing, and nondestructive examination.
These tests are not all repeated before shipment. Check that each report uses the correct method, meets the limit, and identifies the delivered heat or lot. If a hydrostatic or NDT report lacks traceability, hold the material until it is corrected.
Which Documents Must Match the Shipment?
Document review should establish one unbroken chain:
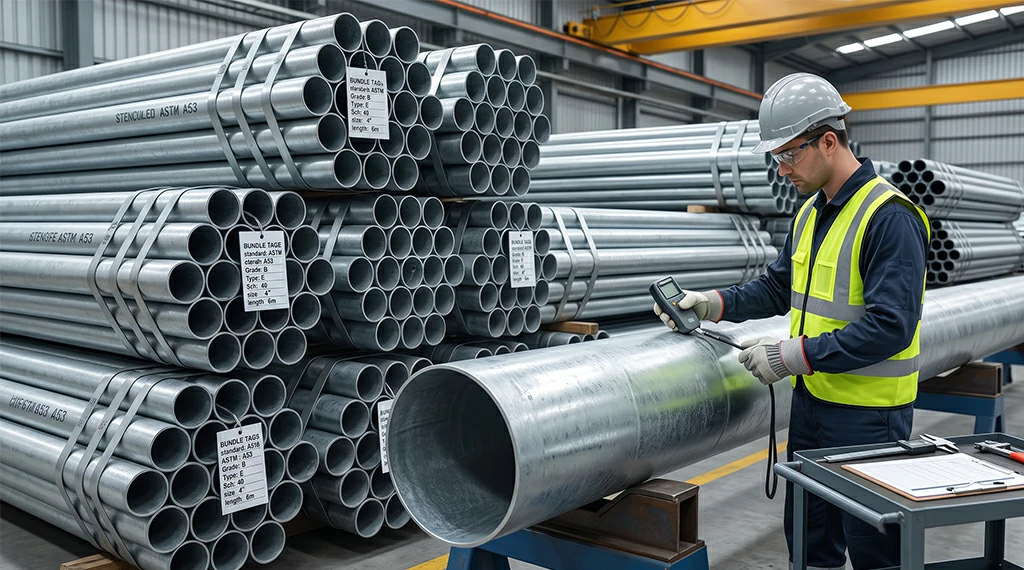
Pipe marking → bundle tag → packing list → MTC → coating report → test report
The MTC should show the manufacturer, standard, grade, heat number, chemistry, mechanical results, and tests. Coating, dimensional, hydrostatic, and NDT reports should use the same traceability reference. Calibration certificates must cover the instruments used.
Use the purchase order as the comparison document. A complete-looking certificate may still refer to the wrong grade, size, standard edition, or coating requirement. When information conflicts, segregate the affected bundles and request a revised document or technical explanation. Do not alter markings or certificates merely to make them agree.
Photographs should connect markings, readings, defects, end protection, and loading condition to a pipe or bundle number. The MTC is often the main link between the delivered pipe and its production data. Buyers who need a closer explanation of heat numbers, chemical composition, mechanical properties, and test results can refer to this guide on how to read a Mill Test Certificate for steel pipes.
How Should the Final Inspection Decision Be Made?
The final report should convert observations into one of four decisions:
- Release: Every mandatory requirement is satisfied and traceable.
- Hold: A result, document, or identity cannot yet be verified.
- Rework and reinspect: The defect can be corrected under the applicable specification.
- Reject: A critical requirement is not met or the defect exceeds the permitted repair scope.
Before release, match quantity and bundle count to the packing list, protect the ends, secure the bundles, and keep material dry. Correct poor packing rather than merely cleaning its visible effects.
Each nonconformity should state the requirement, actual finding, affected quantity, proposed action, and reinspection result. This turns the checklist into a decision record rather than a list of observations.
Repeated defects should also trigger a cause review. Scattered scratches may point to poor handling, while similar bare areas along every weld suggest a process problem. Correcting the cause before repacking or producing the next batch is more useful than repairing the same defect pipe by pipe.
Inspection Support from Baolai Steel
Baolai Steel supplies galvanized steel pipes for construction, water transportation, fire protection, and industrial projects. Buyers can specify the standard, grade, dimensions, zinc requirement, end finish, inspection level, and document package at the quotation stage.
For projects requiring reliable zinc protection and customized pipe solutions, buyers can contact Baolai Steel for support with product selection, technical requirements, inspection coordination, and project documentation. Defining the inspection plan before production helps reduce specification disputes and makes the final release more efficient.
FAQs
How many pipes should be inspected from a shipment?
For visual and workmanship checks, an AQL sampling plan is commonly used. Typical samples are 13 pipes from a lot of 51–90, 20 from 91–150, and 32 from 151–280. Treat each size, grade, or heat as a separate lot. If repeated defects appear, expand the sample or inspect the affected lot in full.
Can repaired zinc coating be accepted?
Yes, provided the applicable specification permits repair. Confirm that the damaged area is within the allowable size, the surface has been properly cleaned, and an approved zinc-rich material or repair method has been used. After the repair has cured or solidified, measure the coating thickness, record the location and result, and reinspect the area before packing. Bundle straps and contact points should not rub against the repaired surface during transport.
What should be done if the coating report is missing?
Place the affected lot on hold rather than accepting it based on appearance. First confirm whether the report was omitted or the required test was never performed. The supplier should provide a report traceable to the relevant pipe, bundle, or production lot. If no valid record exists, arrange approved retesting using the specified method and sampling plan. Release the material only after the results meet the order requirements and traceability has been restored.
How can the internal coating of a long pipe be checked?
Inspect the bore from both ends using adequate lighting, mirrors, or a borescope where required. Select samples from each relevant size, heat, or production lot rather than checking only the most accessible pipes. When the full internal surface cannot be viewed, combine the accessible inspection with coating records, process controls, and any specified destructive verification. If bare areas or irregular coverage are found, expand the sample and hold the affected lot until the extent and cause have been confirmed.


