

A pipe coating inspection should confirm more than colour and surface appearance. Buyers need evidence that the steel was prepared correctly, each coating layer was applied within its process limits, defects were detected, and repairs were retested before shipment. For 3LPE and fusion-bonded epoxy (FBE), the approved inspection and test plan (ITP) should define acceptance criteria.
The most useful inspection begins before production. It connects the pipe specification, coating system, test frequency and documentation into one traceable plan. This guide explains what to check at each stage and what to do when a result is missing or outside the specified limit.
What Should Be Checked Before Coating Begins?
Inspection starts with the purchase specification. It should identify the pipe standard and grade, dimensions, coating type, governing standard and edition, coating class or thickness, cutback length, test frequency and repair procedure.
The inspector should then verify pipe identity and surface condition. Oil, grease, salts, dust, weld spatter and sharp surface defects can weaken adhesion even when the finished coating looks uniform. Welds and pipe ends deserve particular attention because peaks, undercut or rough grinding can leave the coating locally thin.
Surface preparation must follow the specified cleanliness grade and profile. Record ambient conditions, steel temperature and the time between blasting and coating. Buyers comparing different protection systems can review the available coated pipe solutions and define a separate ITP for each system.
How Is 3LPE Coating Inspected During Production?
Three-layer polyethylene is a system rather than a single thick film. It normally consists of an FBE primer, a copolymer adhesive and a polyethylene outer layer. Each layer has a different job, so final total thickness alone cannot prove that the system was applied correctly.
During production, confirm that the prepared pipe remains clean and that application temperatures stay within the qualified procedure. The FBE primer must form a continuous base. The adhesive must bond to both the epoxy and polyethylene, while the PE layer should be even and free from contamination, wrinkles, bubbles, cuts or exposed lower layers.
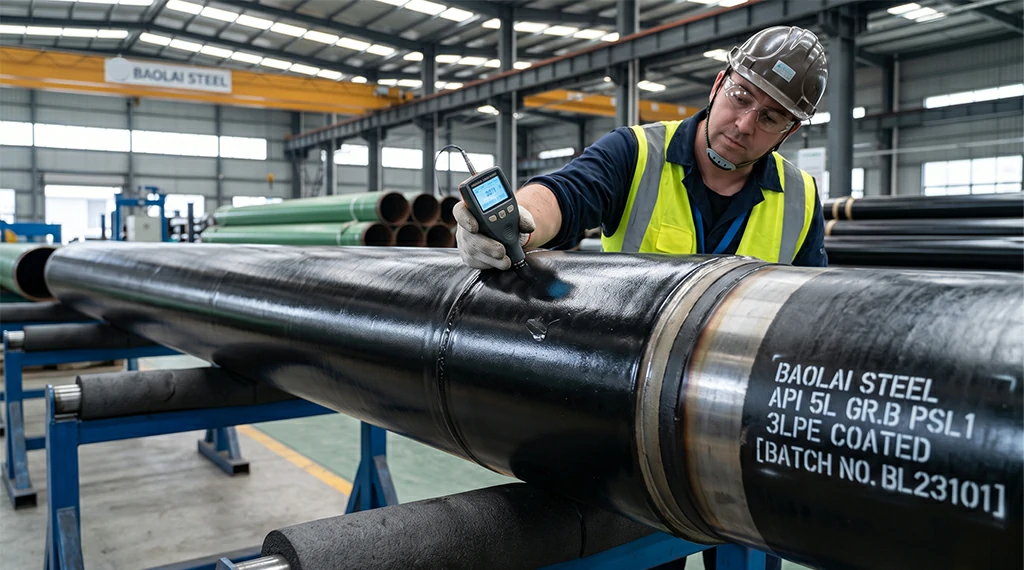
Cooling must not distort the coating or create stress at the cutback. After cooling, check total thickness at the locations and frequency stated in the ITP, including areas near weld seams and pipe ends. The cutback should be clean and dimensionally suitable for welding and the selected field-joint system. These controls are particularly important for factory-applied external coating pipe intended for buried, submerged or mechanically demanding installation.
How Is FBE Coating Inspected?
FBE is applied as an electrostatically charged powder to heated steel. The powder melts, flows and chemically cures into a bonded film. Good performance therefore depends on surface preparation, preheat temperature, powder condition, application uniformity and curing—not simply the final dry film thickness.
Before application, confirm that the powder batch is approved, within shelf life and stored under the manufacturer’s required conditions. During coating, monitor steel temperature and line speed against the qualified procedure. After curing and cooling, inspect for pinholes, blisters, runs, contamination, cracking, incomplete coverage and damage caused by rollers or handling equipment.
Measure thickness around the circumference and along the pipe rather than relying on one convenient reading. Pay particular attention to weld crowns and cutback transitions. The same principles apply to factory-produced FBE coated steel pipe, but the required thickness, test frequency and acceptance limits must come from the governing specification.
Which Tests Are Required for 3LPE and FBE Coatings?
The ITP should distinguish routine production checks from qualification or destructive tests. Routine checks control each pipe or production shift; destructive and laboratory tests usually qualify a material system or represent a defined production lot.
| Test | What it verifies | Appropriate response to failure |
|---|---|---|
| Visual inspection | Coverage, surface defects, cutback condition and handling damage | Mark the area, determine its extent and inspect for hidden discontinuity |
| Thickness measurement | Compliance with minimum, maximum or total thickness requirements | Recheck instrument calibration, expand measurements and isolate affected pipes |
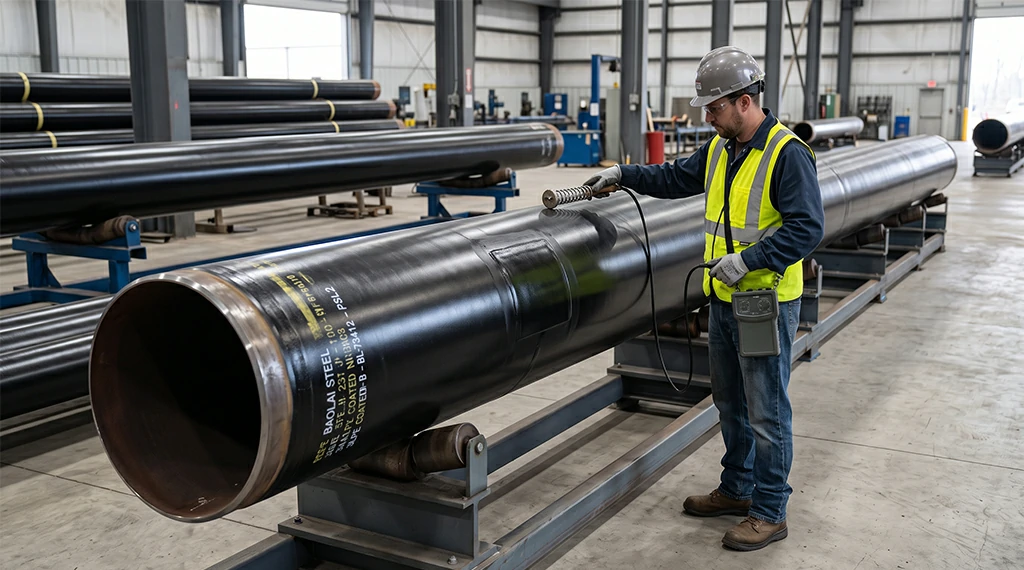
| Holiday detection | Pinholes, cracks or discontinuities that expose the steel | Mark each indication, repair it and repeat the holiday test after curing |
| Adhesion or peel testing | Bond between steel and FBE or between the 3LPE layers | Hold the represented lot and investigate preparation, temperature and material compatibility |
| Impact or indentation testing | Resistance to handling, backfill and installation loads | Review coating class and process control before accepting the lot |
| Cathodic disbondment testing | Resistance to coating separation around a defect under cathodic protection | Treat an excessive result as a system-level problem, not a cosmetic defect |
Test equipment must be suitable for the coating and within calibration. Holiday detector settings, probe type and travel speed should follow the applicable specification and coating thickness; one voltage should not be copied across FBE and 3LPE orders without confirmation. Thickness gauges should be verified on an appropriate reference before use.
Results should record actual values, not only “pass”. Each record should identify the pipe or lot, date, instrument and acceptance limit. The ITP must also define the response to failure: expanded sampling, retesting, reprocessing or rejection. A failed result should not be hidden by averaging it with acceptable values.
How Should Coating Damage and Repairs Be Accepted?
Not every defect requires rejecting an entire pipe, but every repair needs a defined route to acceptance. First compare the damaged area with the maximum repair size and frequency allowed by the project specification. Large, repeated or closely grouped defects may indicate poor process control and should not be treated as isolated handling marks.
The repair area should be cleaned and prepared without damaging sound adjacent coating. Use a repair material approved for the original system and service conditions. Observe its mixing, application, overlap, thickness and curing requirements. A visually smooth patch is not proof of continuity.
After curing, repeat the relevant visual, thickness and holiday checks and record the repair against the pipe identity. If adhesion failure or disbondment extends beyond the visible defect, remove the affected coating until sound material is reached or refer the pipe for reprocessing. Field-joint coating is a separate controlled operation and should be compatible with the factory coating, cutback and installation procedure.
What Documents Should Buyers Review Before Shipment?
The final inspection pack should allow the buyer to trace a result back to the pipe or production lot. At minimum, review the approved ITP, coating material certificates, pipe and batch identification, surface-preparation records, application-temperature records, thickness results, holiday test records, adhesion or peel results where required, repair logs, nonconformance reports and instrument calibration status.
Check whether the records show the specified standard and edition, actual measured values and the applicable acceptance limits. Resolve missing or inconsistent entries before packing. Once pipes are bundled, much of the coating surface becomes inaccessible, while straps, supports and lifting equipment can introduce new damage. Packing should therefore use suitable separators and protected contact points, with repaired areas fully cured before bundling.
Inspection records can confirm whether the applied coating meets the purchase specification, but they cannot correct a coating system that was unsuitable from the beginning. If the coating type has not yet been finalized, compare the main external pipe coating types against the operating temperature, installation method, soil conditions and mechanical damage risk before approving the inspection plan.
FAQs
Can a 3LPE pipe be accepted if the PE layer is damaged but the FBE primer remains intact?
Not automatically. The polyethylene layer provides the mechanical and moisture protection expected from a 3LPE system, so an intact FBE primer does not make the damage acceptable by itself. Compare the affected area with the repair limits in the project specification. If repair is permitted, remove loose material, prepare the surface, apply an approved compatible repair system and restore the required overlap and thickness. Repeat visual, thickness and holiday tests after curing. Damage beyond the permitted size or showing layer separation should be referred for recoating or rejection.
What should be done if a 3LPE peel test fails at only one location?
Hold the production lot represented by the test rather than treating the result as an isolated defect. Check whether the failure occurred between the steel and FBE, between the FBE and adhesive, or between the adhesive and PE, as each points to a different process problem. Review surface cleanliness, pipe temperature, application timing, adhesive batch and cooling records. Conduct expanded peel testing at the locations required by the ITP. Release the lot only if retesting confirms compliance and the cause of the original failure has been identified and controlled.
Can 3LPE and FBE coatings use the same acceptance criteria?
No. Some methods overlap, but the limits are not interchangeable. A 3LPE system is assessed as three bonded layers, including total thickness, peel strength and mechanical resistance. Single-layer FBE is assessed through film thickness, cure, continuity, adhesion and cathodic disbondment.
Confirm the coating system, governing standard and edition before reviewing results. ISO 21809-1 covers three-layer PE and PP systems, while ISO 21809-2 covers external single-layer FBE. Project specifications may impose stricter requirements.
How can buyers confirm that an FBE coating has cured properly?
Colour, hardness and surface appearance alone cannot confirm complete curing. Check whether the pipe temperature, heating time, line speed and cooling records remained within the qualified coating procedure. Where the specification requires it, cure may also be verified using a production test sample and the prescribed thermal or chemical test method. If cure is insufficient, hold the represented pipes because under-cured FBE may have poor adhesion and chemical resistance even when it passes an initial visual inspection. Reheating or acceptance should only follow an approved technical disposition.
Turn Coating Requirements Into a Clear Inspection Plan
Coating disputes often begin before production because the purchase specification does not clearly define thickness tolerances, test frequency, repair limits or traceability requirements. Baolai can review the coating standard, pipe dimensions, service environment and required inspection records, helping identify missing acceptance criteria before they cause delay or rejection.
If your 3LPE or FBE order does not yet have a complete inspection plan, send us your coating inspection requirements. Our team can help align the coating system, test procedures and documentation with the project’s technical and acceptance requirements.


