
Hydrostatic testing checks whether a steel pipe can hold a specified internal pressure without leaking. The pipe is filled with water, pressurized according to the applicable product standard or purchase specification, held for the required time, and inspected for leakage or other unacceptable changes.
The test matters because it provides direct evidence of pressure containment before a pipe is shipped or installed. However, a passing result does not by itself prove corrosion resistance, fatigue life, or long-term suitability for every service. This guide explains how mill hydrostatic testing works, what determines the test conditions, what the result means, and which records international buyers should verify.
What Is Hydrostatic Testing?
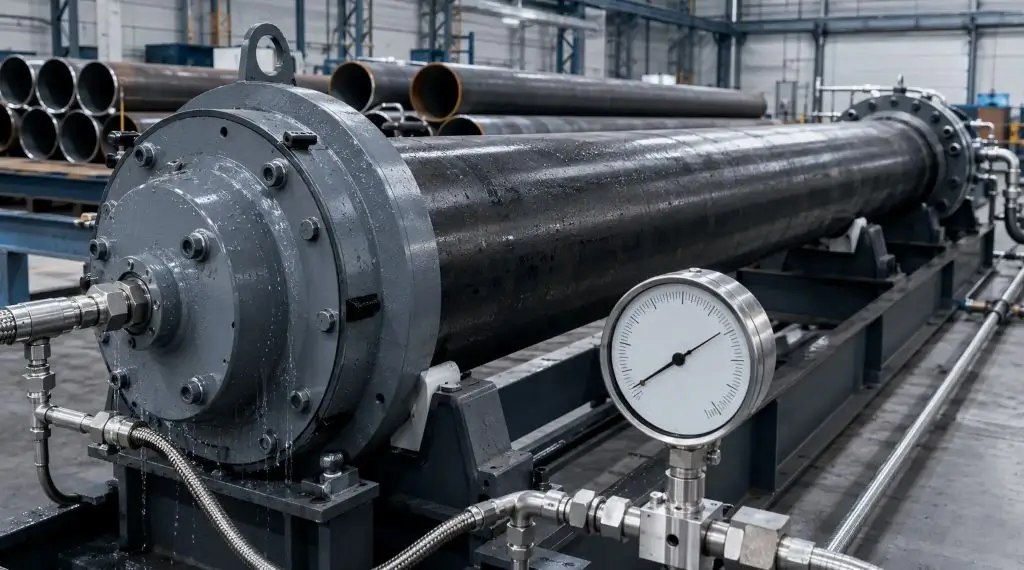
Hydrostatic testing is a controlled quality test in which a pipe is sealed, filled with water or another permitted liquid, and raised to a specified internal pressure. Inspectors then observe the pipe for leakage and any other condition that the applicable standard defines as unacceptable.
Water is commonly used because it is far less compressible than air. Compared with a pneumatic test at the same pressure, this generally limits the stored energy released if a failure occurs. High-pressure water testing still requires trained personnel, suitable equipment, controlled access, and a documented procedure.
The test is important because dimensional checks and visual inspection alone cannot confirm that a pipe will remain leak-tight under internal pressure. A pipe can have acceptable outside diameter, wall thickness, and surface appearance while still containing a through-wall defect or a weld imperfection. This is especially relevant to welded steel pipe options, where the pipe body and weld seam must meet the requirements of the specified product standard.
Finding a problem at the mill is generally less disruptive than discovering it after delivery. Early detection can reduce the risk of rejected materials, replacement freight, site delays, and rework. A traceable test result also gives buyers, engineers, and third-party inspectors evidence that the supplied pipe was evaluated under defined conditions.
The limit of that evidence must remain clear. A passing hydrostatic result shows that the pipe met the stated acceptance criteria under the recorded test conditions. It does not predict decades of corrosion, repeated pressure cycles, external impact, unsuitable installation, or exposure to a different service fluid.
How Steel Pipe Testing Works?
A mill hydrostatic test is more than filling a pipe and watching a pressure gauge. The operator must confirm the correct test conditions, remove factors that could distort the result, observe the relevant parts of the pipe, and connect the final result to the tested material. Although the equipment and acceptance criteria vary by product standard, the process can generally be understood through three stages: preparation and filling, pressurization and inspection, and post-test evaluation and recording.
Prepare and Fill the Pipe
Before testing begins, the operator checks the production order or test plan against the pipe identification. This normally includes the applicable standard and edition, grade, outside diameter, wall thickness, manufacturing method, required pressure, hold time, and acceptance criteria. This step helps prevent a pipe from being tested under conditions intended for another size, grade, or order.
The pipe ends and visible surface are also examined for damage or conditions that could interfere with sealing and inspection. Test heads, pumps, hoses, gauges, relief devices, and safety controls should be suitable for the intended pressure. Where calibration records are required by the quality plan or purchase specification, the gauge identification should be traceable to those records.
The pipe is then sealed and filled with water while trapped air is vented as far as the test arrangement permits. Excess air can store additional energy and make pressure behavior more difficult to interpret. Water quality, drainage, and drying requirements may also need to be considered when the pipe is galvanized, internally coated, or intended for extended storage.
For products such as ASTM A53 ERW welded steel pipes, the test conditions should be taken from the specified standard edition and purchase requirements rather than inferred from the grade name alone.
Pressurize and Hold
Pressure is increased in a controlled manner until the required test value is reached. The hold period should be measured according to the governing procedure, rather than including the time used to raise or stabilize the pressure unless the applicable standard states otherwise.
During the hold period, the operator observes the pipe body and, for welded products, the relevant weld area under the required inspection conditions. The pressure reading is important, but it should not be interpreted in isolation. An apparent pressure change may be related to the pipe, trapped air, temperature variation, equipment condition, or leakage at a test head. Visible water near an end seal must likewise be distinguished from leakage through the pipe itself before a product disposition is made.
A stable gauge reading also does not replace any visual examination required by the applicable procedure. The result should be based on the defined acceptance criteria and the condition of the complete test arrangement.
For fire sprinkler pipe options, buyers should identify the destination, product standard and edition, size and schedule, coating, end connection, required approvals, and inspection-document level. These details help establish whether the proposed testing route matches the project requirement. A general request for “hydro-tested pipe” does not establish the applicable pressure, hold time, permitted alternative methods, or evidence needed for project acceptance.
Inspect, Drain, and Record
After the required hold period, the pressure is released in a controlled manner. The pipe is drained, and any necessary drying or moisture-control measures are completed according to the product specification, coating requirements, storage plan, or agreed procedure.
The result should then be connected to the tested pipe, batch, or other production identity used by the applicable quality system. Depending on the order requirements, the record may include the actual test pressure, hold time, test date, result, pipe or batch identification, equipment reference, inspector, and witness information.
If the result is abnormal, the affected material should be identified and evaluated before release. The investigation may need to distinguish a pipe-body or weld-seam defect from leakage at the temporary sealing equipment. Whether repair and retesting are permitted depends on the governing product standard and purchase specification. Where they are permitted, the disposition and subsequent result should remain traceable. Any purchaser or third-party witnessing requirements are best agreed before production so that the inspection can be scheduled and documented correctly.
What Sets Hydrostatic Test Pressure?
The pressure question should begin with the test scope, not a multiplier. A mill hydrostatic test evaluates individual pipe lengths before shipment. A field hydrostatic test evaluates an assembled system, including site joints and other installed components. These tests answer different acceptance questions and are normally governed by different documents.
This distinction explains why some buyers have heard “1.5 times” in connection with hydrostatic pressure. Some system codes or project specifications use a multiplier, subject to their own conditions. It should not be copied into a mill pipe enquiry without checking the governing document. For mill testing, the product standard and edition usually set the calculation basis, limits, and hold time; dimensions, grade, and manufacturing route may also affect the value.
| Buyer Decision | Why It Changes the Requirement | What to Provide or Verify |
| Is this a mill or field test? | It identifies the test object and governing document. | State whether acceptance covers individual pipe lengths or the installed system. |
| Which standard and edition apply? | Editions may define different calculations, limits, hold times, or permitted alternatives. | Quote the full designation and edition shown in the project specification or purchase order. |
| Which pipe is being tested? | Size, wall thickness, grade, and manufacturing route may affect the required test value. | Provide NPS or OD, wall thickness or schedule, grade, and seamless or welded construction. |
| Are supplementary requirements needed? | Witnessing or purchaser-defined conditions affect production planning. | Identify the inspection party, document level, and project clauses before production. |
| What proves compliance? | A pressure value without traceability cannot reliably be matched to the delivered material. | Require consistent pipe, heat, batch, size, grade, and test-record identification. |
For a fire protection project specifying ASTM A795, the selected ASTM A795 ERW fire sprinkler pipe must still match the required size, schedule, coating, end connection, and documents. The official ASTM A795/A795M-21 summary says each length is hydrostatically tested without pipe-wall leakage, but permits a nondestructive electrical alternative when accepted by the purchaser. The applicable edition and purchaser decisions therefore matter.
ASTM, API, EN, ISO, AS/NZS, GOST, and project requirements should be checked individually. Additional pressure, witnessing, or document requirements should be confirmed against the product standard and stated before production.
How Buyers Verify Test Results?
A simple statement such as “hydro tested” may not provide enough evidence for project acceptance. The buyer should first compare the reported test with the contract: Was the correct standard and edition used? Does the record identify the same grade, outside diameter, wall thickness, heat, batch, or pipe numbers as the delivered material? Are the pressure unit and hold time clearly stated?
A verification package may include the standard, product identification, test pressure, hold time, date, result, gauge or calibration reference, and witness details when required. The goal is to obtain enough evidence for project acceptance without requesting records the project does not use.
The hydrostatic record should agree with the MTC. This guide on how to read a mill test certificate for steel pipes explains how to match heat numbers, grades, dimensions, and test references. Inconsistencies are best clarified before shipment.
A pass normally means that the pipe met the specified leakage-related acceptance criteria under the recorded test conditions. It should not be presented as proof of corrosion resistance, fatigue life, coating performance, or fitness for an operating condition that was never evaluated.
If a pipe does not meet the criteria, it should be identified and investigated under the applicable quality procedure. A leak may come from the pipe body, weld seam, test head, or temporary seal. Repair and retesting depend on the product standard and purchase specification; where permitted, the disposition and retest should remain traceable.
Conclusion: Specify the Test Correctly
Hydrostatic testing is useful only when the test conditions and records answer the buyer’s actual acceptance question. The test scope, product standard and edition, pressure, hold time, acceptance criteria, and material identification must correspond with one another. Buyers should therefore ask not only whether the pipe was hydrostatically tested, but also whether the proposed test and documentation route match the project specification.
Project documents do not always contain every detail needed to place an order. A BOQ may identify the pipe size without stating the required test documents, while a datasheet may refer to a standard without clarifying its edition, witnessing requirements, or permitted testing alternatives. For buyers sourcing welded, seamless carbon steel, coated, or fire protection pipes, Baolai Steel can help review these requirements against the proposed product and quality-control route. Buyers can provide the available BOQ, pipe schedule, datasheet, destination, and inspection clauses to clarify their steel pipe hydrostatic testing requirements and identify missing or conflicting details before they create inspection, acceptance, or delivery problems.
FAQs
1. Do Structural Pipes Need Hydrotesting?
Not automatically. A hollow structural section is primarily specified for carrying external loads, while a pressure pipe is selected to contain a fluid. Products that look similar can therefore follow different standards and acceptance tests. If a structural pipe will also carry pressurized fluid, the engineer should specify a product and testing route suitable for that combined duty. A supplier should not assume that a structural designation proves pressure tightness.
2. Can Test Water Affect Coatings?
It can if the water, test duration, drainage, or drying process is incompatible with the coating or lining. Hydrostatic testing may be scheduled before or after coating depending on the product specification and project plan. For internally coated, galvanized, or specially lined pipe, the buyer should confirm water-quality limits, exposure restrictions, inspection requirements, and drying procedures with the coating specification. Coating integrity should not be inferred from the pipe’s hydrostatic result.
3. When Should Stored Pipe Be Retested?
Long storage or transport does not automatically mean every pipe must be hydrostatically retested. The decision depends on the contract, storage environment, visible corrosion or damage, loss of traceability, original test records, and the requirements of the engineer or inspection authority. If damage is suspected, the material should first be isolated and assessed. The appropriate response may be visual inspection, dimensional checks, NDT, or hydrostatic retesting, depending on the identified risk and governing specification.


